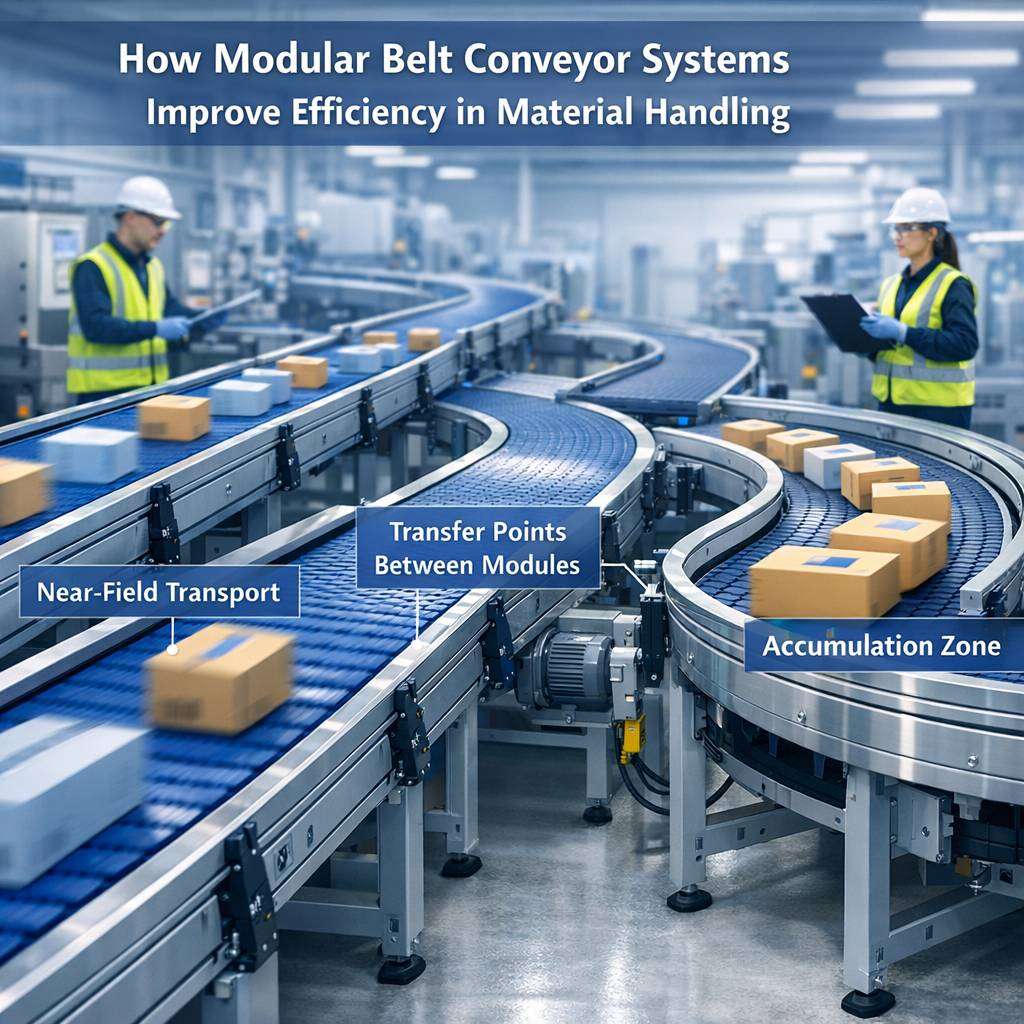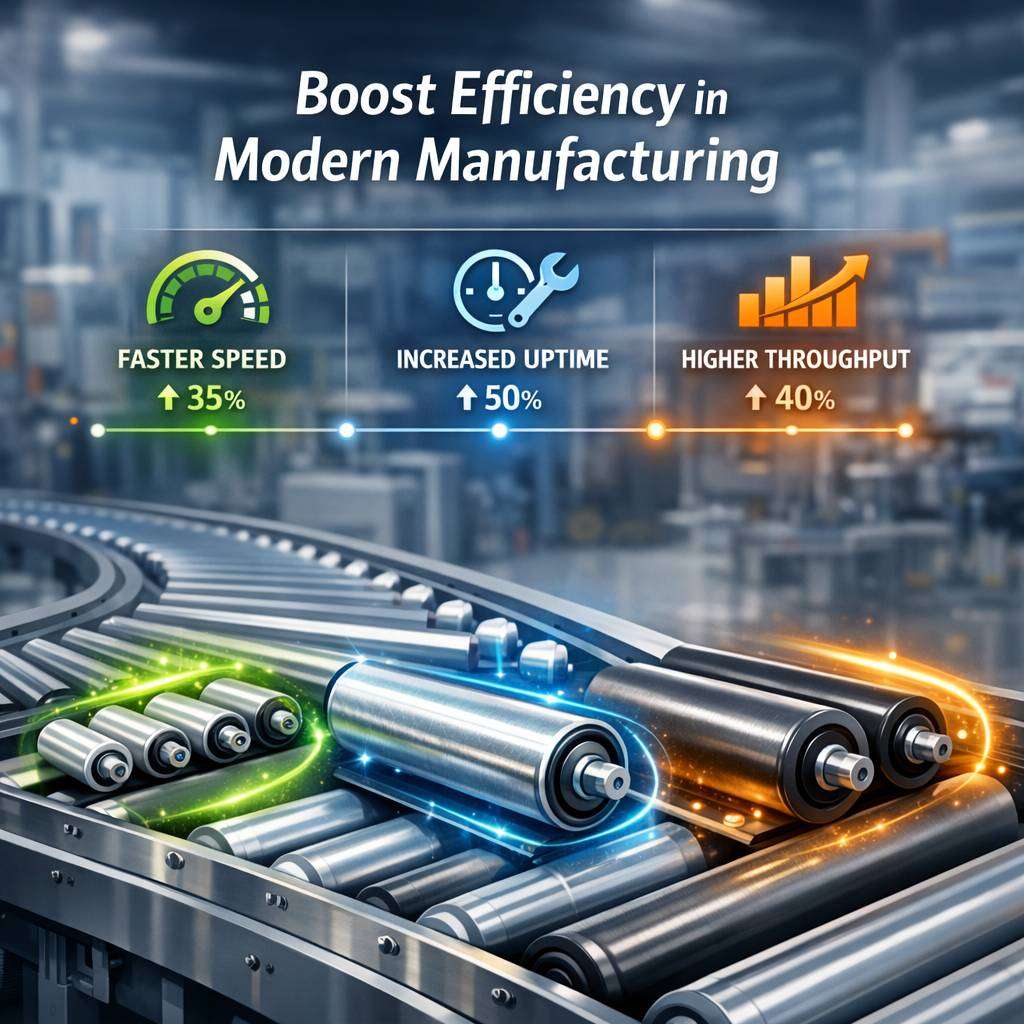


Looking for an efficient conveyor system? Explore the innovative UVCS V3.0 LED Conveyor System designed to enhance your manufacturing process. This reliable conveyor offers precise control, durability, and seamless integration, making it ideal for various industrial applications. Upgrade your production line today with this advanced conveyor solution for improved efficiency and productivity.
Conveyors are essential in modern manufacturing and logistics, streamlining the movement of goods efficiently. They reduce manual labor and increase productivity, making operations smoother. To find high-quality conveyor solutions, visit https://conveyorrollers.co.uk for reliable and durable conveyor products tailored to your needs.
In today’s fast-paced industrial environment, selecting the right conveyor system is crucial to optimise workflow efficiency, reduce labour costs, and enhance safety. With a broad range of conveyor types and configurations available, making an informed decision can seem overwhelming. This guide aims to provide a comprehensive overview to help you identify the ideal conveyor solution tailored to your specific business needs. Whether you operate in manufacturing, logistics, food processing, or any other sector, understanding the fundamentals and the options available is key to making a confident choice.
Understanding Conveyor Systems
Conveyor systems are mechanical devices designed to transport materials or products from one location to another within a facility. They play an essential role in automating processes, minimising manual handling, and increasing throughput. Modern conveyor systems come in diverse forms, each suited to different kinds of payloads, environments, and operational requirements.
When considering conveyor systems for your business, it’s important to assess factors such as the nature of goods, space constraints, budget, and desired speed. A well-chosen conveyor can streamline operations and increase overall productivity.
Types of Conveyors
Choosing the right conveyor begins with understanding the various types available. Here are some of the most common conveyor types:
- Roller Conveyors: Ideal for heavy or bulky items, especially boxes or pallets. They use rollers mounted in frames to facilitate easy movement.
- Belt Conveyors: Equipped with a continuous belt, these conveyors are suitable for transporting a variety of items, including irregularly shaped goods and fragile products.
- Chain Conveyors: Often used in industrial settings for transporting heavy items, these systems use linked chains to move products along defined paths.
- Flat Plate Conveyors: Similar to belt conveyors but with a solid surface, suitable for transporting items that might fall through a belt.
- Incline and Decline Conveyors: Designed to transport products vertically or across ramps, saving space and facilitating flow control.
- Vertical Conveyors: Used to move materials between different levels or floors within a facility.
Choosing the right type depends largely on your product specifications and the operational environment.
Key Factors to Consider When Choosing Conveyors
Selecting a conveyor system requires careful consideration of multiple factors to ensure it aligns with your operational needs:
Product Characteristics
- Size and Weight: Heavier or larger items may require reinforced roller or chain conveyors.
- Shape and Material: Fragile or irregularly shaped products might be best suited for belt conveyors with specialised surfaces.
- Sensitivity: Delicate products need gentle handling, influencing the type of conveyor chosen.
Space and Layout
- Available Space: Compact conveyors are essential for constrained environments.
- Flow Path: Decide on straight runs, curves, inclines, or declines based on your plant layout.
- Integration: Ensure compatibility with existing equipment and workflows.
Conveyor FAQ
What is a conveyor?
A conveyor is a mechanical device used to transport materials or objects from one location to another, commonly used in manufacturing, packaging, and distribution facilities. Conveyors can be powered or manual and come in various types depending on the application.
What are the different types of conveyors?
There are several types of conveyors, including:
- Roller Conveyors: Use rollers to move items; ideal for heavy or palletised loads.
- Belt Conveyors: Employ a continuous belt for smooth transportation of goods.
- Chain Conveyors: Use chains to move large or heavy objects, often in industrial settings.
- Gravity Conveyors: Rely on gravity to move items downhill; suitable for light loads.
- Slider Bed Conveyors: Use a flat surface to slide items along.
- Turntable Conveyors: Enable items to change direction on a rotating platform.
How do I choose the right conveyor for my business?
Choosing the right conveyor depends on factors such as the type and size of the items to be transported, the required speed, load capacity, space availability, and environmental conditions. Consulting with conveyor specialists can help identify the most suitable system for your needs.
What are the benefits of using a conveyor system?
Conveyor systems increase efficiency by automating material handling, reduce labour costs, improve safety by minimising manual lifting, and streamline workflow processes. They can also handle large volumes of items quickly and consistently.
How much does a conveyor system cost?
The cost of a conveyor system varies widely based on type, length, capacity, features, and customisation needs. Basic models might start from a few hundred dollars, while industrial systems can cost several thousand or more. It’s best to get quotes from suppliers tailored to your specific requirements.
How can I maintain my conveyor system?
Regular maintenance includes inspecting for wear and tear, lubricating moving parts, adjusting components for proper alignment, cleaning to prevent dust and debris buildup, and replacing worn-out parts promptly. Following the manufacturer’s maintenance guidelines ensures longevity and optimal performance.
Are conveyors suitable for all industries?
Conveyors are versatile and can be adapted to many industries such as manufacturing, warehousing, food processing, pharmaceuticals, and packaging. However, specific applications may require specialised conveyor types that meet industry standards for hygiene, safety, or environmental conditions.
Can conveyors be customised?
Yes, conveyors can be customised to meet specific operational needs, including size, shape, speed, load capacity, and integration with other equipment. Custom options ensure the conveyor system fits seamlessly into your existing workflow.
How long does it take to install a conveyor system?
Installation time varies based on the complexity of the system and site conditions. Simple conveyor setups might take a few hours to a day, while larger, more complex systems could require several days or weeks. Planning and coordination with installers are essential for an efficient setup.
Who should I contact for conveyor system solutions?
You should reach out to specialised conveyor manufacturers or system integrators who can assess your needs, offer customised solutions, and provide installation and maintenance services. Research reputable providers with experience in your industry for the best results.
A conveyor system streamlines manufacturing, ensuring efficient movement of items and reducing manual labor. Implementing advanced automation enhances safety and productivity. For more information on cutting-edge solutions, visit https://www.conveyor.com/platform/security-questionnaire-automation-software.
Operational Requirements
- Speed and Throughput: Determine the desired conveyor speed to achieve optimal production rates.
- Flexibility: Consider modular conveyors for adaptable workflows.
- Frequency: High-frequency operations may require more durable systems with less downtime.
Environmental Conditions
- Temperature and Humidity: Certain conveyor components are more suitable for harsh environments.
- Cleanliness: Food processing or pharmaceutical industries demand easy-to-clean, hygienic conveyor systems.
Budget and Maintenance
- Initial Investment: Balance cost with durability and operational longevity.
- Maintenance Needs: Opt for systems that minimise downtime through reliable componentry and accessibility.
Benefits of Modern Conveyor Systems
Investing in the right conveyor system can translate into numerous operational advantages:
- Increased efficiency through automated material handling.
- Reduced labour costs and human errors.
- Enhanced safety by minimising manual lifting and handling.
- Improved consistency and product quality.
- Greater flexibility in production scheduling.
Customisation and Integration
Many conveyor solutions can be customised to fit specific industry requirements. Whether you need specialised transfer points, sorting mechanisms, or integration with robotics and automated packaging lines, modern conveyor systems are flexible. Collaborating with manufacturers or specialists can help tailor a conveyor for optimal performance.
Maintenance and Support
Proper maintenance is vital to ensuring the longevity of your conveyor systems. Regular inspections, lubrication, and cleaning can prevent breakdowns. Additionally, choosing systems from reputable suppliers that offer comprehensive support, spare parts, and training can save your business time and money in the long run.
Future Trends in Conveyor Technology
As technology advances, conveyor systems continue to evolve. Innovations such as sensors for real-time monitoring, automation integration, and smart control systems optimise efficiency further. Lightweight yet durable materials and environmentally friendly designs are also becoming more prevalent, reducing operational costs and environmental impact.
By understanding the various conveyor options and considering the specific demands of your business, you can select a conveyor system that significantly enhances your operational efficiency. Whether upgrading existing infrastructure or implementing new solutions, making informed choices ensures your investment adds lasting value to your operations.
Conveyors are essential in streamlining manufacturing and packaging processes, increasing efficiency and reducing labor costs. They come in various types, including belt, roller, and chain conveyors, tailored to different industries and applications. Investing in a high-quality conveyor system ensures smooth operation, safety, and durability. For reliable conveyor solutions, visit https://www.jorgensenconveyors.com/. Their expertise in conveyor design and installation helps businesses optimize their production lines and improve overall productivity.