

Conveyors play a crucial role in modern manufacturing and logistics, streamlining processes and enhancing efficiency. They allow for the seamless movement of goods and materials across various stages of production. Choosing the right conveyor system can significantly impact operational productivity. For a reliable and versatile solution, consider exploring the X65 plastic chain conveyors, which are designed to meet diverse needs. Check them out here: https://www.flexlink.com/en/solutions/product/x65-plastic-chain-conveyors.
In today’s fast-paced world, efficiency is the key to success in many industries. One of the unsung heroes of this efficiency is the conveyor system. These mechanical devices are designed to transport materials from one place to another, making processes smoother and more efficient. In this article, we will explore the various types of conveyors, their uses across different sectors, and the multitude of benefits they offer, all while unpacking the compelling reasons to integrate conveyor systems into your operations.
Types of Conveyor Systems
Conveyor systems come in various types, each specifically designed to handle specific materials and cater to a range of industrial needs. Understanding these types can help you select the most appropriate system for your requirements.
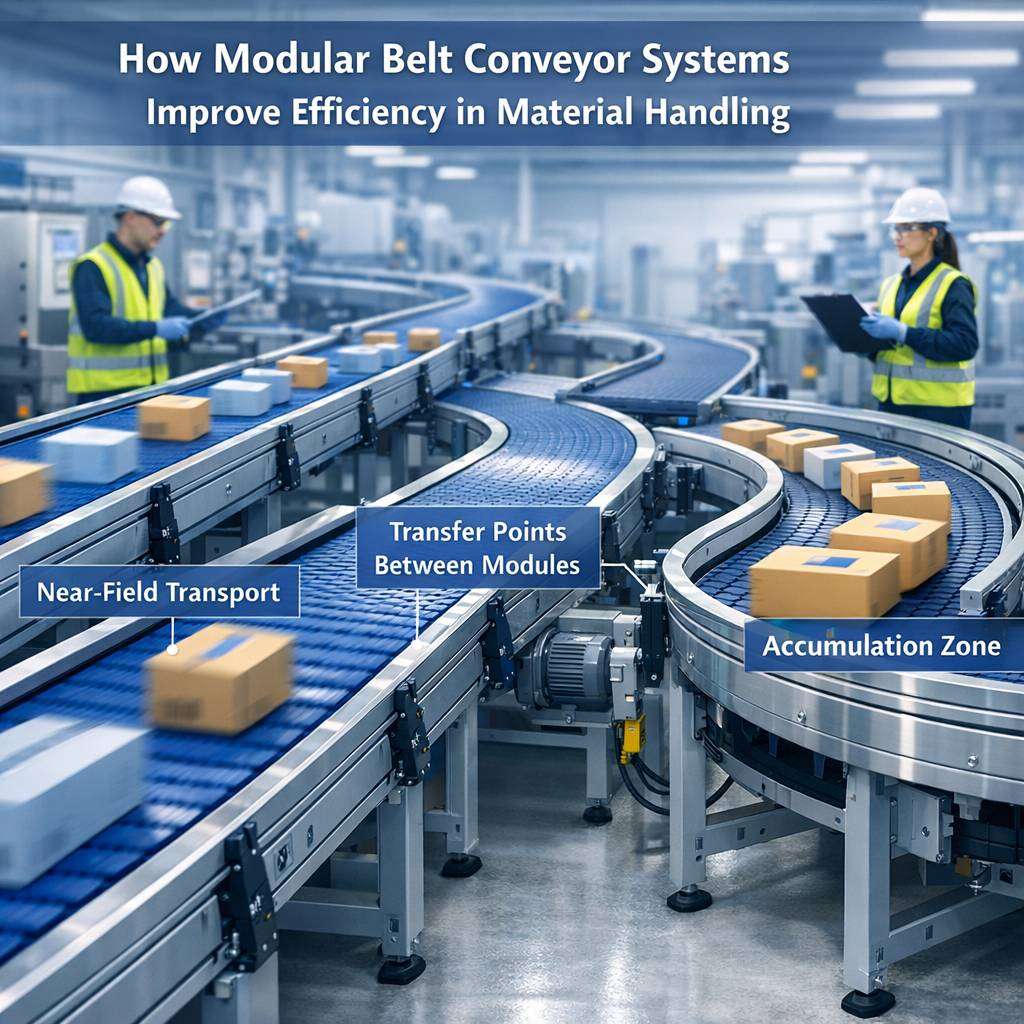
One of the most common types is the belt conveyor, which consists of a continuous loop of material that carries items from one point to another. Its versatility allows it to transport anything from small packages to heavy machinery, making it ideal for industries such as manufacturing, retail, and logistics.
Another popular choice is the roller conveyor, which utilises a series of rollers to facilitate the movement of goods. This type of conveyor is particularly useful in distribution centres and warehouses for moving heavier loads. The roller system also allows for easy manual intervention, making it an efficient option for sorting and marshalling items.
For specific applications, one might consider screw conveyors. These are particularly effective for handling bulk materials, especially in industries such as agriculture and food processing. The spiralling shaft within a tube moves the materials forward, making it an ideal solution for transporting powders, granulates, and slurries.
The magnetic conveyor is another example, which is perfect for handling ferrous materials. Incorporating magnets into the conveyor system allows for efficient movement of metal components without them falling off during transit. This method of transportation is particularly valuable in automotive and metalworking industries.
Finally, there are overhead conveyor systems, which are perfect for businesses requiring vertical transport. Utilising the overhead space efficiently, these conveyors can transport goods in a more organised way, allowing for optimal floor space usage. They are commonly used in assembly lines or in paint shops, where products must be painted while suspended.
Conveyors play a crucial role in modern logistics and manufacturing, efficiently moving materials from one location to another. For innovative conveyor solutions, explore the offerings at https://www.asgco.com/ for optimal performance.
Uses of Conveyor Systems
ConVEYor systems serve an array of industries, each tailored to meet specific operational needs. In the manufacturing sector, they play a crucial role in streamlining assembly lines, where components must move smoothly from one work station to another, enhancing productivity and reducing the risk of human error.
Logistics and warehousing benefit immensely from conveyor systems, making the process of sorting and transporting items faster and more accurate. With the rise of e-commerce, the demand for efficient order fulfilment has only increased, and conveyor systems serve as the backbone of this modern supply chain.
In the food and beverage industry, hygiene is paramount, and here, conveyor systems demonstrate their adaptability by offering stainless steel options that meet stringent health and safety standards. These conveyors allow for the smooth movement of products while ensuring compliance with strict sanitation requirements.
Pharmaceutical manufacturers also rely on conveyor systems to move delicate materials throughout production facilities. This sector demands precision, and automated conveyor systems help in maintaining consistent quality while reducing handling times.
Conveyor FAQ
What is a conveyor?
A conveyor is a mechanical device used to transport materials from one location to another. It typically consists of a belt, rollers, or chains that move items along a fixed path and can be found in various industries such as manufacturing, packaging, and distribution.
What are the different types of conveyors?
There are several types of conveyors, including:
- Belt Conveyors: Utilise a continuous loop of material to transport goods.
- Roller Conveyors: Use rollers placed at intervals for moving items down the line.
- Chain Conveyors: Employ chains for heavy-duty transportation of bulk materials.
- Screw Conveyors: Rotate a helical screw blade to move granular or powdery materials.
- Magnetic Conveyors: Use magnets for transporting ferrous products.
How do I choose the right conveyor for my application?
Choosing the right conveyor depends on several factors:
- The type and weight of materials being transported
- The distance over which they need to be moved
- The layout and space available in your facility
- Speed requirements and operational conditions (e.g., wet or dry environments)
- Budget
Consulting with an experienced supplier or engineer can help identify the best solution.
What maintenance is required for conveyors?
Regular maintenance is essential for optimal performance and longevity. Key tasks include:
- Inspecting belts, rollers, chains, and other components regularly.
- Keeping the equipment clean to prevent debris buildup.
- Lubricating moving parts as needed according to manufacturer recommendations.
- Checking alignment and tension on belts or chains.
Implementing these practices can minimise downtime and enhance efficiency.
Can conveyors be customised?
Yes! Many manufacturers offer customised solutions tailored to specific needs. Options include adjustments in size, speed, material selection (such as food-grade belts), modular configurations that suit unique layouts, adding accessories like sensors or guides, etc.
Where are conveyors commonly used?
Conveyors are widely utilised across various sectors like:
- Manufacturing (for assembly lines)
- Warehousing (for order fulfillment)
- Distribution centers (for shipping processes)
- Food processing plants (for transporting ingredients)
Their capability allows businesses to streamline operations effectively regardless of industry type.
Are conveyors energy efficient?
Many modern conveyor systems feature energy-efficient designs that consume less power during operation compared to older models. Additionally, utilising variable speed drives allows operators more control over energy usage depending on workflow demands—contributing positively towards sustainability efforts within industrial settings.
If you have any more questions about conveyors not covered here or specific needs relating them – don’t hesitate reaching out!
Benefits of Conveyor Systems
Integrating conveyor systems into your operations brings forth a myriad of advantages that can greatly enhance overall efficiency. Firstly, reducing manual labour is one of the most significant benefits. Automated systems lessen the physical strain on employees, allowing your workforce to focus on higher-value tasks. This can lead to increased job satisfaction and lower employee turnover.
Conveyor systems also boost productivity by facilitating continuous movement of goods, which minimises downtime between processes. This continuous flow helps to speed up production and reduces lead times for deliveries. Additionally, with the ability to connect different parts of a production line seamlessly, these systems contribute to a more organised workflow.
Safety is an important consideration in any workplace, and conveyor systems can enhance safety standards significantly. By automating material handling, the risk of accidents associated with manual lifting or carrying goods is drastically reduced. Furthermore, modern conveyor systems come equipped with safety features, such as emergency stops and safety barriers, which protect both the employees and the equipment.
The versatility of conveyor systems is another notable benefit. With a variety of types and customisation options available, businesses can create systems that fit specific space constraints and operational requirements. This adaptability ensures that they can evolve alongside your business needs, incorporating new technologies or expanding existing operations without the need for a complete overhaul.
Lastly, conveyor systems can contribute to significant cost savings over time. The initial investment may appear daunting, but the efficiency gains, reduced labour costs, and improved throughput can lead to substantial long-term savings, enhancing the bottom line.
In summary, conveyor systems offer more than just transportation of goods; they are a fundamental component of modern industrial operations. By understanding the different types, applications, and advantages, businesses can make informed decisions to integrate these systems effectively and reap the rewards of enhanced efficiency and productivity.
Conveyors play a vital role in modern logistics, enhancing efficiency and productivity. Businesses looking to optimize their operations can explore various conveyor options at https://conveyorrollers.co.uk. With robust designs and reliable performance, conveyors streamline processes, making material handling smoother and faster across industries.
Conveyors have revolutionized material handling in various industries, enhancing efficiency and productivity. By utilizing a conveyor, businesses can seamlessly transport goods, reducing manual labor and minimizing operational costs. Investing in high-quality conveyor systems ensures reliable performance and longevity, essential for any modern production environment.
Conveyors are essential in modern manufacturing, streamlining processes and boosting efficiency. From sorting products to transporting materials, these systems help reduce labor costs and minimize errors. For top-notch conveyor solutions, visit https://conveyor-automation.com/. Investing in the right conveyor technology can significantly enhance productivity and optimize your operations for better output.