

In modern manufacturing and logistics, efficiency is the key to success. One of the most effective ways to enhance operational processes is through the utilisation of horizontal belt conveyors. These systems have revolutionised the way materials are transported within various industries. With a variety of configurations like modular belt conveyors, chain-driven belt conveyors, and roller belt conveyors, they are integral to achieving streamlined operations. This article explores the top advantages of implementing horizontal belt conveyors in your operations.
Enhanced Efficiency and Productivity
Horizontal belt conveyors are designed to maximise the efficiency of material handling processes. By facilitating the smooth and continuous transportation of goods, these systems minimise downtime and ensure a steady flow of materials. Unlike manual handling methods, which are subject to human error and fatigue, a belt conveyor system can operate round the clock without breaks. This continuity translates into enhanced productivity, allowing companies to meet high demand swiftly.
Versatility in Application
One of the standout characteristics of horizontal belt conveyors is their versatility in applications across various industries. Whether it’s food processing, packaging, or automotive manufacturing, these systems can be easily tailored to fit specific needs. For instance, modular belt conveyor systems provide the adaptability required for handling a wide range of product sizes and weights. As such, businesses can invest confidently in belt conveyors for sale, knowing they will suit multiple purposes and applications.
Flexible Configuration Options
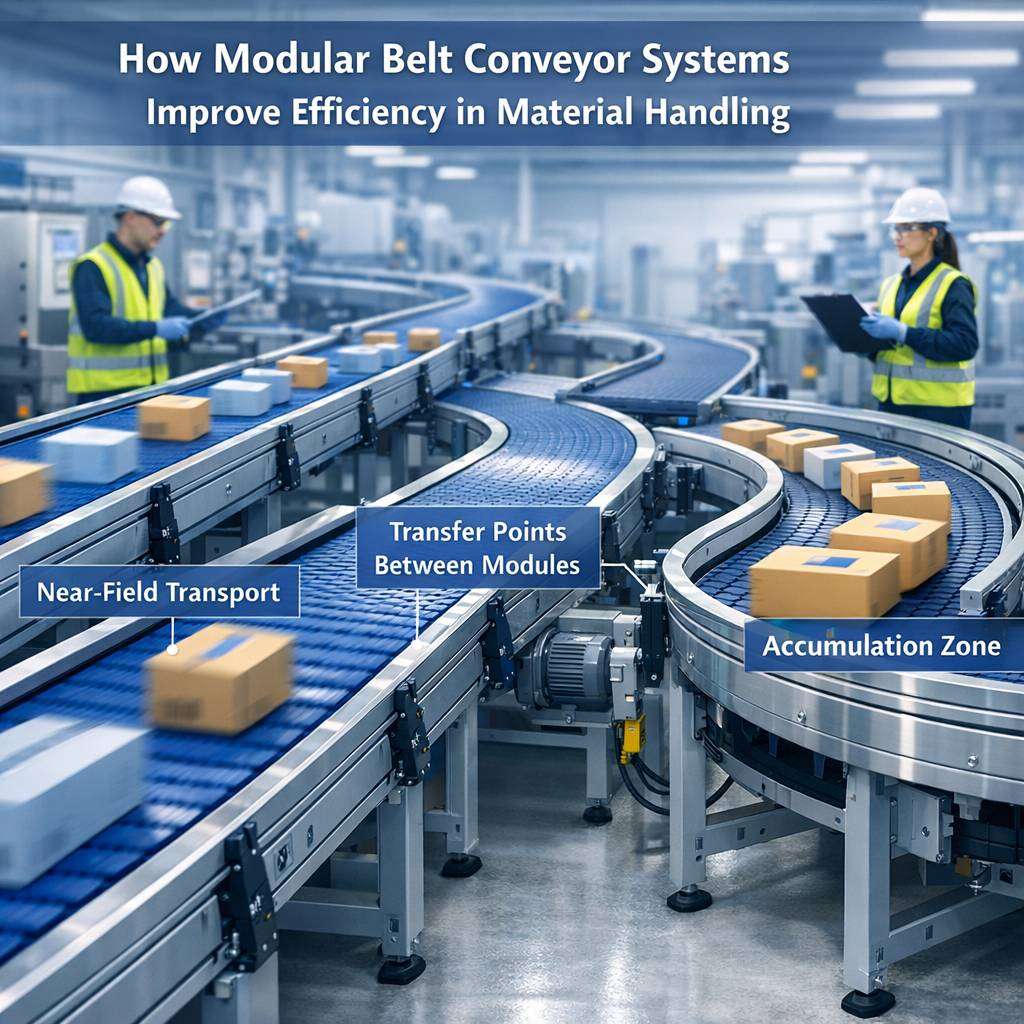
The design of horizontal belt conveyors allows for flexible configuration options that can be customised to fit specific operational layouts. For example, modular belt conveyors can be configured in straight, curved, or inclined paths, making them suitable for both small and large spaces. This flexibility ensures that materials can be moved efficiently around obstacles or around the factory floor. Additionally, businesses benefit from the ability to re-configure their conveyor systems easily as operational requirements evolve.
Reduced Labour Costs
Implementing horizontal belt conveyors significantly reduces labour costs associated with material handling. Traditionally, moving large quantities of products required a substantial workforce. By employing an efficient belt conveyor system, companies can decrease their reliance on manual labour, allowing personnel to focus on more complex tasks that require human intervention. The reduction in labour costs not only improves profit margins but also enhances employee satisfaction by reallocating resources to more engaging work.
Improved Safety Standards
Safety is paramount in operational environments, and horizontal belt conveyors contribute positively to this aspect. By mechanising the process of moving materials, these conveyors minimise the risks of workplace injuries often associated with manual handling. Additionally, many modern systems come equipped with built-in safety features such as emergency stop buttons and guards to prevent accidents. This focus on safety not only protects employees but also fosters a safer work environment, enhancing overall operational efficiency.
Consistent Material Flow
Another significant advantage of using horizontal belt conveyors is their ability to provide a consistent material flow. Unlike manual processes, which can experience fluctuations and variability, a belt conveyor ensures that materials are delivered at a steady rate. This consistency is crucial for maintaining efficiency in production lines, as it helps to prevent bottlenecks and delays. The result is a more streamlined workflow that supports timely product delivery.
Low Maintenance Requirements
Modern horizontal belt conveyor systems are designed for durability and low maintenance. With materials engineered to withstand wear and tear and easy-to-replace components, these systems require minimal upkeep compared to other systems. Chain-driven belt conveyors, for example, are built to be robust and reliable, while modular belt conveyors can be quickly repaired or segments replaced. This reduction in maintenance not only saves time but also reduces long-term operational costs.
Space Efficiency
Horizontal belt conveyors can be designed with a compact footprint, making them suitable for operations with limited space. This space efficiency allows businesses to maximise their operational layouts without sacrificing functionality. Additionally, these systems can often be integrated seamlessly with other equipment, such as packing stations or sorting systems, providing a cohesive workflow that optimises space utilisation.
A horizontal belt conveyor offers a streamlined solution for material handling in various industries. Designed for efficient transportation, these conveyors minimize space while maximizing productivity. Whether for transporting bulk materials or packaged goods, their versatility can enhance workflow. For a reliable selection of horizontal belt conveyors, visit https://conveyorrollers.co.uk and explore your options today.
Environmental Considerations
As businesses continue to seek ways to reduce their environmental impact, horizontal belt conveyors can contribute positively. Many manufacturers offer eco-friendly options that utilise energy-efficient motors and materials, thus reducing energy consumption. Furthermore, the longevity and durability of these systems minimise waste and the need for replacements. By choosing the right conveyor system, organisations can align their operations with sustainable practices.
Customisation and Scalability
Lastly, one of the prime advantages of horizontal belt conveyors lies in their customisation and scalability. Whether you are a small start-up or a large manufacturer, conveyor systems can be customised to meet your specific operational needs. As your business grows, your conveyor system can be scaled up or adapted without significant overhauls. This flexibility ensures that investments in belt conveyor systems remain viable in the long term, catering to evolving business demands.
In summary, the integration of horizontal belt conveyors into operational processes offers a multitude of advantages, from increased efficiency and flexibility to enhanced safety and environmental responsibility. As companies continue to adapt to the complexities of modern manufacturing and logistics, the strategic implementation of these systems can be pivotal in achieving sustainable growth and competitive advantage.